7 Tips for North American Bearing Certification?
North American Bearing Certification is becoming a practical trust signal, not merely a document in a supplier’s folder. Buyers now examine material traceability, dimensional control, heat treatment, lubrication, and testing records. The 2023 ISO Survey reported more than 1.26 million ISO 9001 certificates worldwide, showing how widely formal quality systems are used. Meanwhile, the U.S. International Trade Administration continues to identify industrial machinery as a major manufacturing and export sector. Bearings sit quietly inside that system. Their failure does not stay quiet.
Reports from Grand View Research and MarketsandMarkets also connect bearing demand with automation, electric vehicles, wind power, and predictive maintenance. These applications raise expectations for repeatable performance. A certificate alone cannot prove that every shipment is reliable. It must connect to controlled processes, competent laboratories, and evidence that an auditor can actually follow.
W. Edwards Deming, a leading quality-management expert, said, “In God we trust; all others must bring data.” That principle fits bearing certification closely. A strong application should show calibrated gauges, lot numbers, inspection results, and corrective-action records. Small details matter. A smudged heat-treatment record may create a large customer question.
The seven tips ahead focus on standards, documentation, testing, supplier evidence, and audit readiness across North American markets. Requirements can differ by product, customer, and application. That is easy to underestimate. Even experienced teams should verify current ABMA, ASTM, ANSI, ISO, and customer-specific requirements before making a compliance claim. Certification is useful, but disciplined evidence makes it believable.
Identify the Applicable North American Bearing Standards and Certification Bodies
North American bearing certification starts with the correct standard, not a generic quality certificate. Tip 1: Define the bearing type, load, speed, material, and intended market. Radial and thrust bearings may follow different tolerance requirements. Tip 2: Compare ANSI/ABMA dimensional standards with ISO 492 or ISO 199. They often align, but acceptance limits and test language can differ. Tip 3: Request the latest controlled editions. Old drawings create expensive confusion.
Tip 4: Separate product certification from quality-system certification. ISO Survey 2023 reported 1,265,174 ISO 9001 certificates worldwide. That number shows broad quality-system adoption, but ISO 9001 alone does not prove bearing accuracy or fatigue life. Tip 5: Select a certification body accredited for the required scheme. In the United States, verify accreditation through the ANSI National Accreditation Board. In Canada, check the Standards Council of Canada framework. The certificate should name the tested product scope, facility, standard, and surveillance cycle.
Tip 6: Build a technical file with material certificates, heat-treatment records, dimensional reports, lubricant details, and traceable test results. ASTM’s 2023 annual reporting notes more than 12,000 consensus standards, so “ASTM compliant” is incomplete without a specific designation. Tip 7: Audit the laboratory’s competence under ISO/IEC 17025. A practical warning: supplier declarations can look polished while missing measurement uncertainty. I have seen that gap delay approval. Recheck sampling plans, because one perfect bearing cannot represent an uncontrolled production batch.
Verify Product Specifications, Materials, and Manufacturing Requirements
7 Tips for North American Bearing Certification?
Bearing certification is not one universal certificate. It is evidence that product specifications, materials, and manufacturing controls match the buyer’s requirements. ISO 492 defines dimensional and running accuracy classes, while ISO 281 supports basic rating-life calculations.
Tip 1:
Confirm the exact load, speed, clearance, tolerance, and lubrication requirements.
Tip 2:
Request signed drawings and revision-controlled specifications.
Tip 3:
Check whether calculations use realistic loads, contamination, and operating temperatures.
Materials deserve physical proof.
Tip 4:
Review mill certificates for steel chemistry, heat treatment, hardness, and cleanliness.
Tip 5:
Match the heat number on the report with the bearing or production lot.
A certificate without batch traceability is weak evidence. ASTM test methods can support chemical, hardness, and fatigue-related verification. Small gaps matter.
Manufacturing records reveal practical reliability.
Tip 6:
Inspect dimensional reports, roundness, surface finish, internal clearance, and runout.
Tip 7:
Audit process controls for grinding, washing, assembly, sealing, and final inspection.
The U.S. Department of Energy’s Motor Systems Market Assessment reports that motor-driven equipment uses about 70% of industrial electricity. Poor bearing fit can increase friction, heat, and maintenance exposure. That figure is broad, not bearing-specific. Still, it shows why verification matters.
I would also request nonconformance records and corrective-action history. Perfect paperwork can hide imperfect production.
Complete Testing, Factory Audits, and Certification Application Procedures
North American bearing certification requires more than passing a laboratory test. It demands controlled testing, transparent factory audits, and complete application records. Start by defining the bearing’s use, load range, speed, temperature, and expected service life. These details guide the test plan and prevent unsuitable evidence.
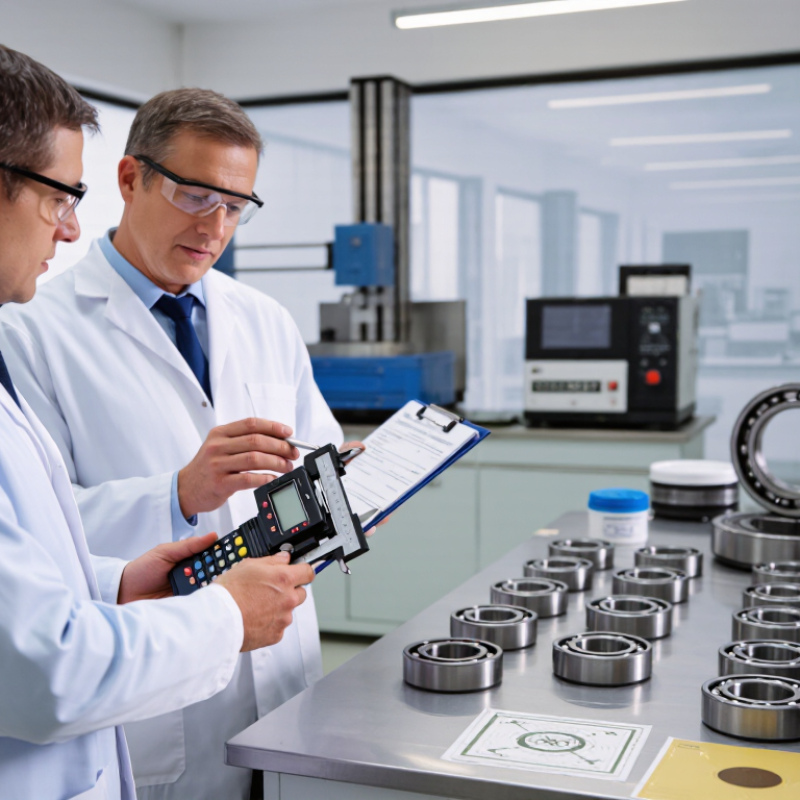
Tip 1: Test representative samples. Measure dimensions, hardness, vibration, noise, friction, and fatigue performance. Record the batch number, test equipment, operator, and environmental conditions. Calibration certificates should remain current and traceable. Small details matter. An independent, competent laboratory can strengthen technical credibility, especially when results may face regulatory or customer review.
Tip 2: Prepare the factory before an audit. Auditors may inspect incoming materials, heat treatment, grinding, assembly, lubrication, packaging, and final inspection. Keep process instructions visible and quality records easy to retrieve. Operators should understand inspection limits, not merely follow signatures. A clean production floor helps, but documented control matters more. The weak point is often supplier traceability. Corrective actions should include owners, deadlines, and verification evidence.
Tip 3: Treat the certification application as a technical file. Include drawings, specifications, risk evaluations, test reports, audit responses, quality procedures, and product labels. Check that every document uses the same model numbers and revision dates. Requirements can vary by product and market, so confirm them with the responsible certification body. It is tempting to submit early. That can create avoidable delays when one missing record reopens the review.